Pre-shipment inspection for plastic homeware is most useful when it confirms a buyer-approved product and packing standard. It is not a generic photo exercise or a promise that every item is identical. This guide explains how retail buyers can define a practical inspection scope, use AQL-based sampling appropriately, and turn the findings into a clear shipment decision.
1. Define what the inspection needs to decide
A pre-shipment inspection is not a substitute for product development. Its job is to help the buyer decide whether finished goods and packing match the agreed requirement closely enough to release, rework, hold, or investigate. Start by writing that decision in plain language. For example: 'Confirm that the finished drawer-organiser set matches the approved sample, the agreed pack count, and the specified carton markings before shipment release.'
The scope should match the risk. A simple open basket may need close attention to moulding appearance, sharp edges, dimensions, count, and carton protection. A clip-lid storage set may also need closure action, gasket presence, component fit, and stack stability. A tumbler can introduce additional checks for assembly, closure, care information, and visible decoration. One generic list cannot cover every homeware product without leaving meaningful gaps.
Agree who will read the report and what they need to see. A retail buyer may require a concise release recommendation, while a product-development team needs photos against the approved standard and a list of recurring defects. Logistics may focus on carton dimensions, count, marks, and loading condition. Designing the report for the decision maker makes the inspection evidence more useful than a long, unprioritised photo folder.
2. Assemble one approved reference pack before inspection
The inspection starts with a complete reference pack. Include the approved product sample, component or colour standard, product specification and drawing where relevant, retail-pack sample, approved artwork, barcode and label instructions, master-carton marking, purchase order, and the buyer's defect definitions. If the source pack is incomplete, the inspector may be forced to make assumptions that the buyer and supplier would not make themselves.
Version control matters. State the approval date and version in the documents. A production line may have an old image, a changed colour, or a later packaging revision available at the same time. The buyer should identify the version that represents the order being inspected. This protects the inspection from becoming a debate about which email attachment was authoritative.
For a multi-SKU range, include a SKU-by-SKU summary. It should show product name, visible colour, expected components, quantity per retail pack, quantity per inner pack, quantity per master carton, and the specific functions that need checking. This lets the inspection sample cover the actual range rather than over-focusing on the most visible product.
| Reference item | What it proves | Typical inspection use |
|---|---|---|
| Approved sample | Visual and functional benchmark | Compare colour, finish, fit, and operating action |
| Packing sample | Retail presentation and protection | Verify count, inserts, sleeve or box, and barcode area |
| Carton mark | Receiving and shipping instruction | Confirm SKU, quantity, orientation, and buyer marks |
3. Use AQL sampling as an agreed method, not a magic number
Acceptance Quality Limit, commonly called AQL, is a way to set a sample size and acceptance or rejection threshold for lot-by-lot inspection. ISO 2859-1 describes sampling schemes indexed by AQL for inspection by attributes. In practical buyer terms, it helps a team inspect a defined sample from a production lot consistently instead of making a release decision from a few convenient pieces.
AQL does not mean that a certain percentage of defects is automatically acceptable to every buyer, product, or market. The plan must define the lot, inspection level, sample size, defect categories, and acceptance criteria. Critical safety or legal issues generally need a separate rule from visible cosmetic variation. Major functional defects may need a different threshold from minor finish variation. Those definitions belong in the buyer-supplier agreement, not in an inspector's improvised judgement.
Before the order is finished, agree how the plan applies to each SKU and what happens if a finding is above the agreed limit. The action may be rework, additional sorting, a re-inspection, a shipment hold, or another buyer-approved response. The inspection report should explain what was found, how the sample was selected, and which agreed criterion led to the recommendation.
4. Check the functions and defects that matter for plastic homeware
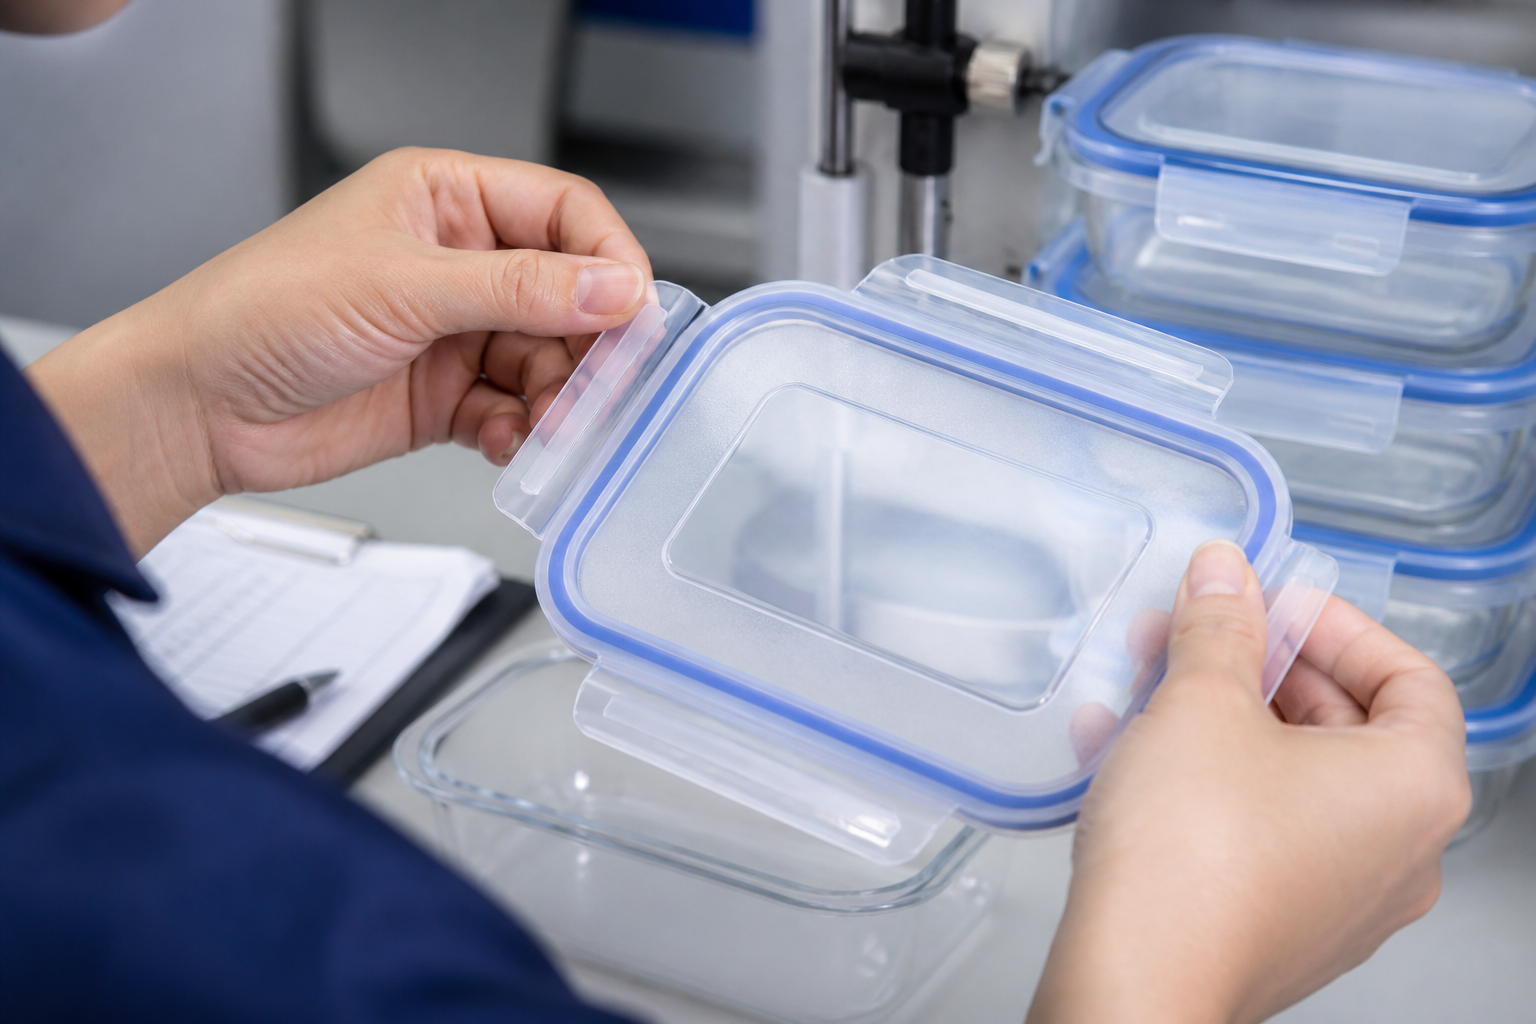
Start with the product's intended function. For a drawer organiser, check dimension, flatness where relevant, nesting, edges, visible surface, and whether pieces sit together as specified. For a storage container, inspect body and lid fit, gasket or clip presence, closure action, component alignment, nesting or stacking, and visible moulding quality. For a cleaning caddy, check handle feel, drainage feature, assembled parts, and whether accessories fit the intended location.
Use the buyer-approved sample to describe what counts as a defect. Terms such as 'minor scratch' or 'poor colour' are too vague on their own. Where possible, show photographs of acceptable and unacceptable appearance, define which viewing distance or surface area matters, and state whether the issue affects safety, function, retail presentation, or all three. This makes factory testing more repeatable and helps a rework team focus on the actual release requirement.
Do not ignore product identity. Inspect correct SKU, visible colour, component combination, decoration, and set count alongside the physical condition. A perfectly moulded item in the wrong colour or a retail pack missing one part is still an order problem. Product identity and packing count checks are especially important where several similar variants share a production line.
5. Inspect retail packs, inner packs, and master cartons
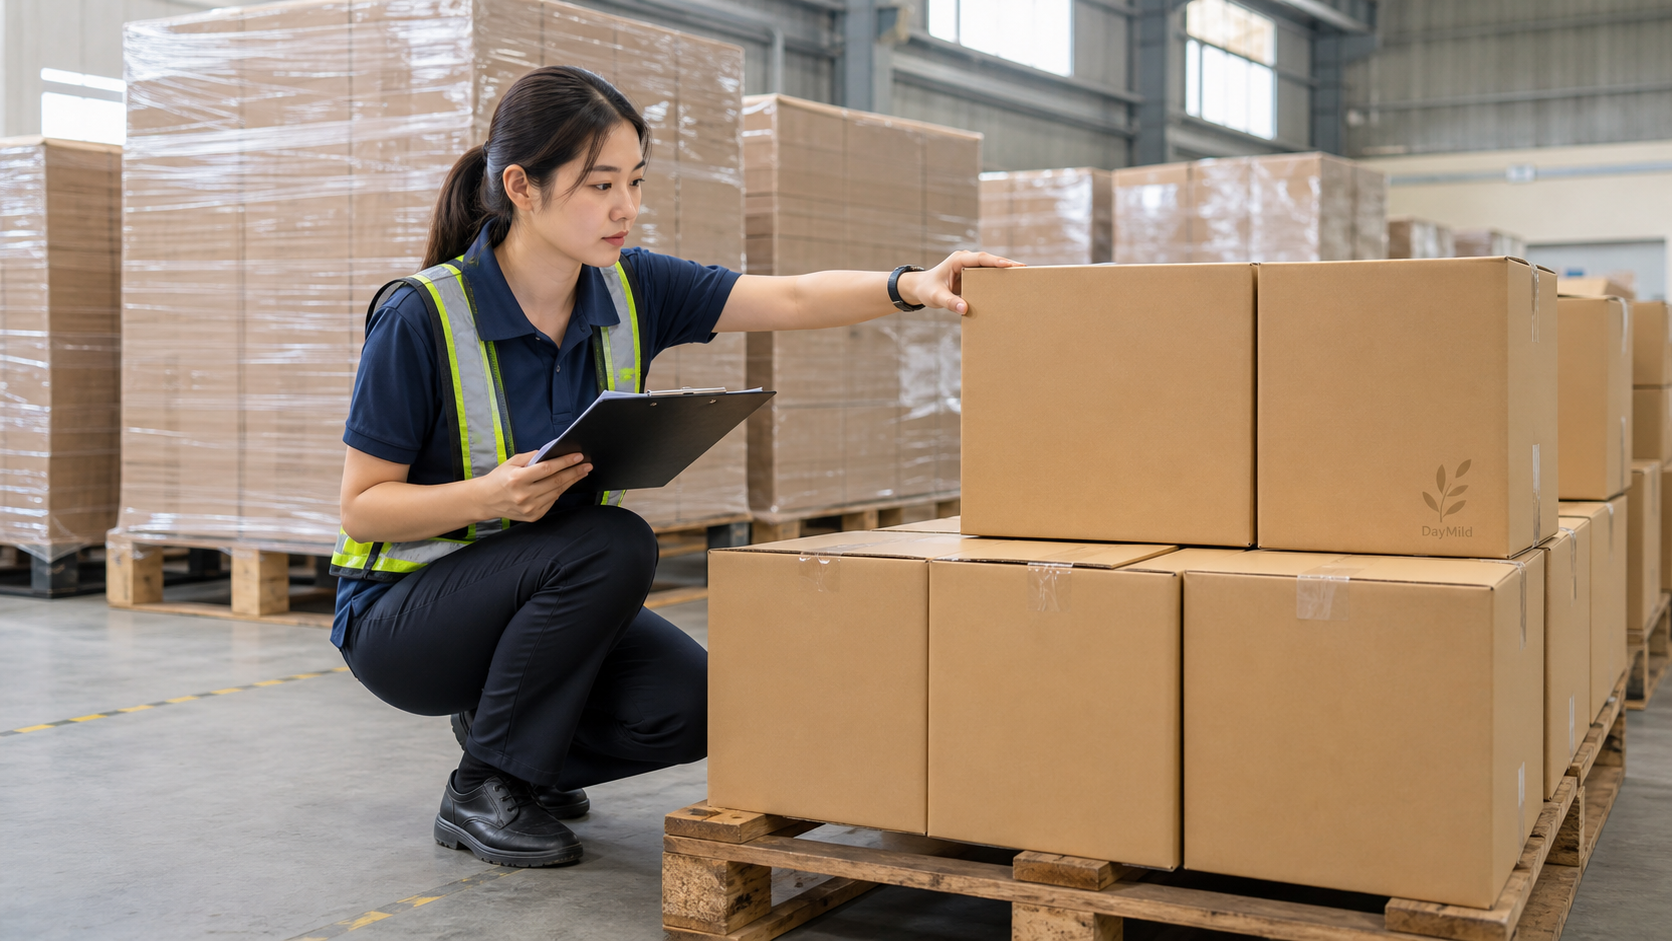
The product must arrive in the same condition in which it was inspected. That makes packing part of the inspection rather than a final administrative detail. Review the retail pack for correct product, visible information, item count, protective material, and obvious damage. Then move outwards: check inner-pack count, orientation, separator use, master-carton count, carton seal, carton marks, and any retailer-specific label requirement.
Carton measurements and weights may matter to a buyer's receiving process, freight plan, or retail distribution system. Record them against the agreed document when required. If cartons are overfilled, under-protected, or marked incorrectly, the issue can affect handling even when the individual product is acceptable. Photograph a representative selection of cartons and any area where damage, crushing, moisture, or incorrect printing is observed.
For loading or pallet verification, confirm the buyer's agreed requirements before the activity. Depending on the contract and Incoterm, responsibility for packing, inspection, transport, and documentation can sit with different parties. The objective is not to assign blame in the report; it is to verify that the order meets the agreed handoff requirements before goods leave the control of the supplier.
6. Turn findings into a clear shipment decision
A useful report separates observation from decision. List the sample size, inspection date, location, product versions, reference documents, and checks completed. Then group findings by defect type and severity according to the buyer-approved plan. Photos should show enough context to identify the SKU, component, and issue without becoming a gallery of unlabelled close-ups.
When a finding needs action, document the proposed corrective route and who approves it. Rework may require a defined sorting method, replacement components, revised pack, or additional inspection. A buyer should know whether the issue is contained, whether the corrected goods will be rechecked, and whether the release condition has changed. This is more constructive than a binary 'pass/fail' note that leaves the next step unclear.
Keep the language factual. An inspection sample can support a decision on the lot under the agreed plan; it cannot prove that every uninspected piece is identical. Likewise, a passed functional check supports the specific sample and condition tested, not a broad consumer-performance claim. Clear scope protects the buyer, supplier, and end customer.
7. Use inspection learning in the next product brief
The best use of an inspection report is to improve the next order. If repeated scuffing appears at a carton corner, examine the pack orientation and separation. If lids are inconsistent, review component fit, assembly control, and the approved closure reference. If carton marks cause receiving confusion, simplify the carton specification and approval process. A recurring issue is often a signal that the original brief was incomplete rather than that inspection needs more photos.
Share the learning across product, packaging, and sourcing teams. A visible product defect may originate in a material finish decision. A crushed retail pack may originate in carton configuration. A missing part may originate in an unclear set-count instruction. Keeping the original reference pack, report, and corrective action together makes the next development cycle more efficient.
For new food-storage or private-label home organisation programmes, pair the inspection plan with a stronger source brief. DayMild's guide to food storage containers for retail explains how material, closure, documentation, and pack choices affect the product review. The private-label home organisation guide shows how to define assortment and packaging roles before production.
8. Prepare an inspection brief before goods are complete
Send the inspection brief early enough for the supplier and inspector to prepare the correct reference material. Include the purchase order, SKU list, approved sample and pack photos, product specification, packing and carton instructions, inspection timing, defect definitions, and required report format. If the order includes several product families, say which functions are critical for each one.
State the decision rule. Explain who receives the report, whether the buyer requires a release recommendation, who can approve rework, and whether a re-inspection is expected after corrective action. This avoids a common last-minute problem: a detailed report arrives, but nobody has agreed what happens if a nonconformity is found.
If you are preparing an initial DayMild enquiry, you can start smaller. Tell us the product category, target market, approximate quantity, and the product and packing checkpoints your team considers important. We can help you identify which details should be fixed in the approved brief before factory testing or shipment inspection is scheduled.
Frequently asked questions
What is AQL in a pre-shipment inspection?
AQL is an acceptance-sampling approach that uses an agreed lot size, sample size, and acceptance or rejection criteria for attribute inspection. It helps teams inspect consistently but must be adapted to the product and buyer-approved defect definitions.
Does a passed AQL inspection guarantee every item is defect-free?
No. Sampling supports a decision about a lot under an agreed inspection plan. It does not prove that every uninspected unit is identical or create a broad performance guarantee.
What should be checked on plastic homeware before shipment?
The checklist should follow the product, but commonly includes product identity, visible finish, sharp edges, dimensions where fit matters, function, component presence, pack count, retail packaging, carton condition, and required markings.
When should pre-shipment inspection take place?
Schedule it when finished goods and retail packing are sufficiently complete for a representative review, while there is still time to address an agreed corrective action before release.
Conclusion: inspect against an agreed reference
AQL-based inspection is most valuable when the buyer, supplier, and inspector work from the same approved product-and-pack reference. Define the functions, visual tolerances, packing route, defect categories, and release action before goods are ready to leave the factory.
Send DayMild your product category, destination market, and required inspection checkpoints to begin a sourcing conversation that is clear about both the product and the shipment handoff.